White Vinegar Making Equipment and Turnkey System
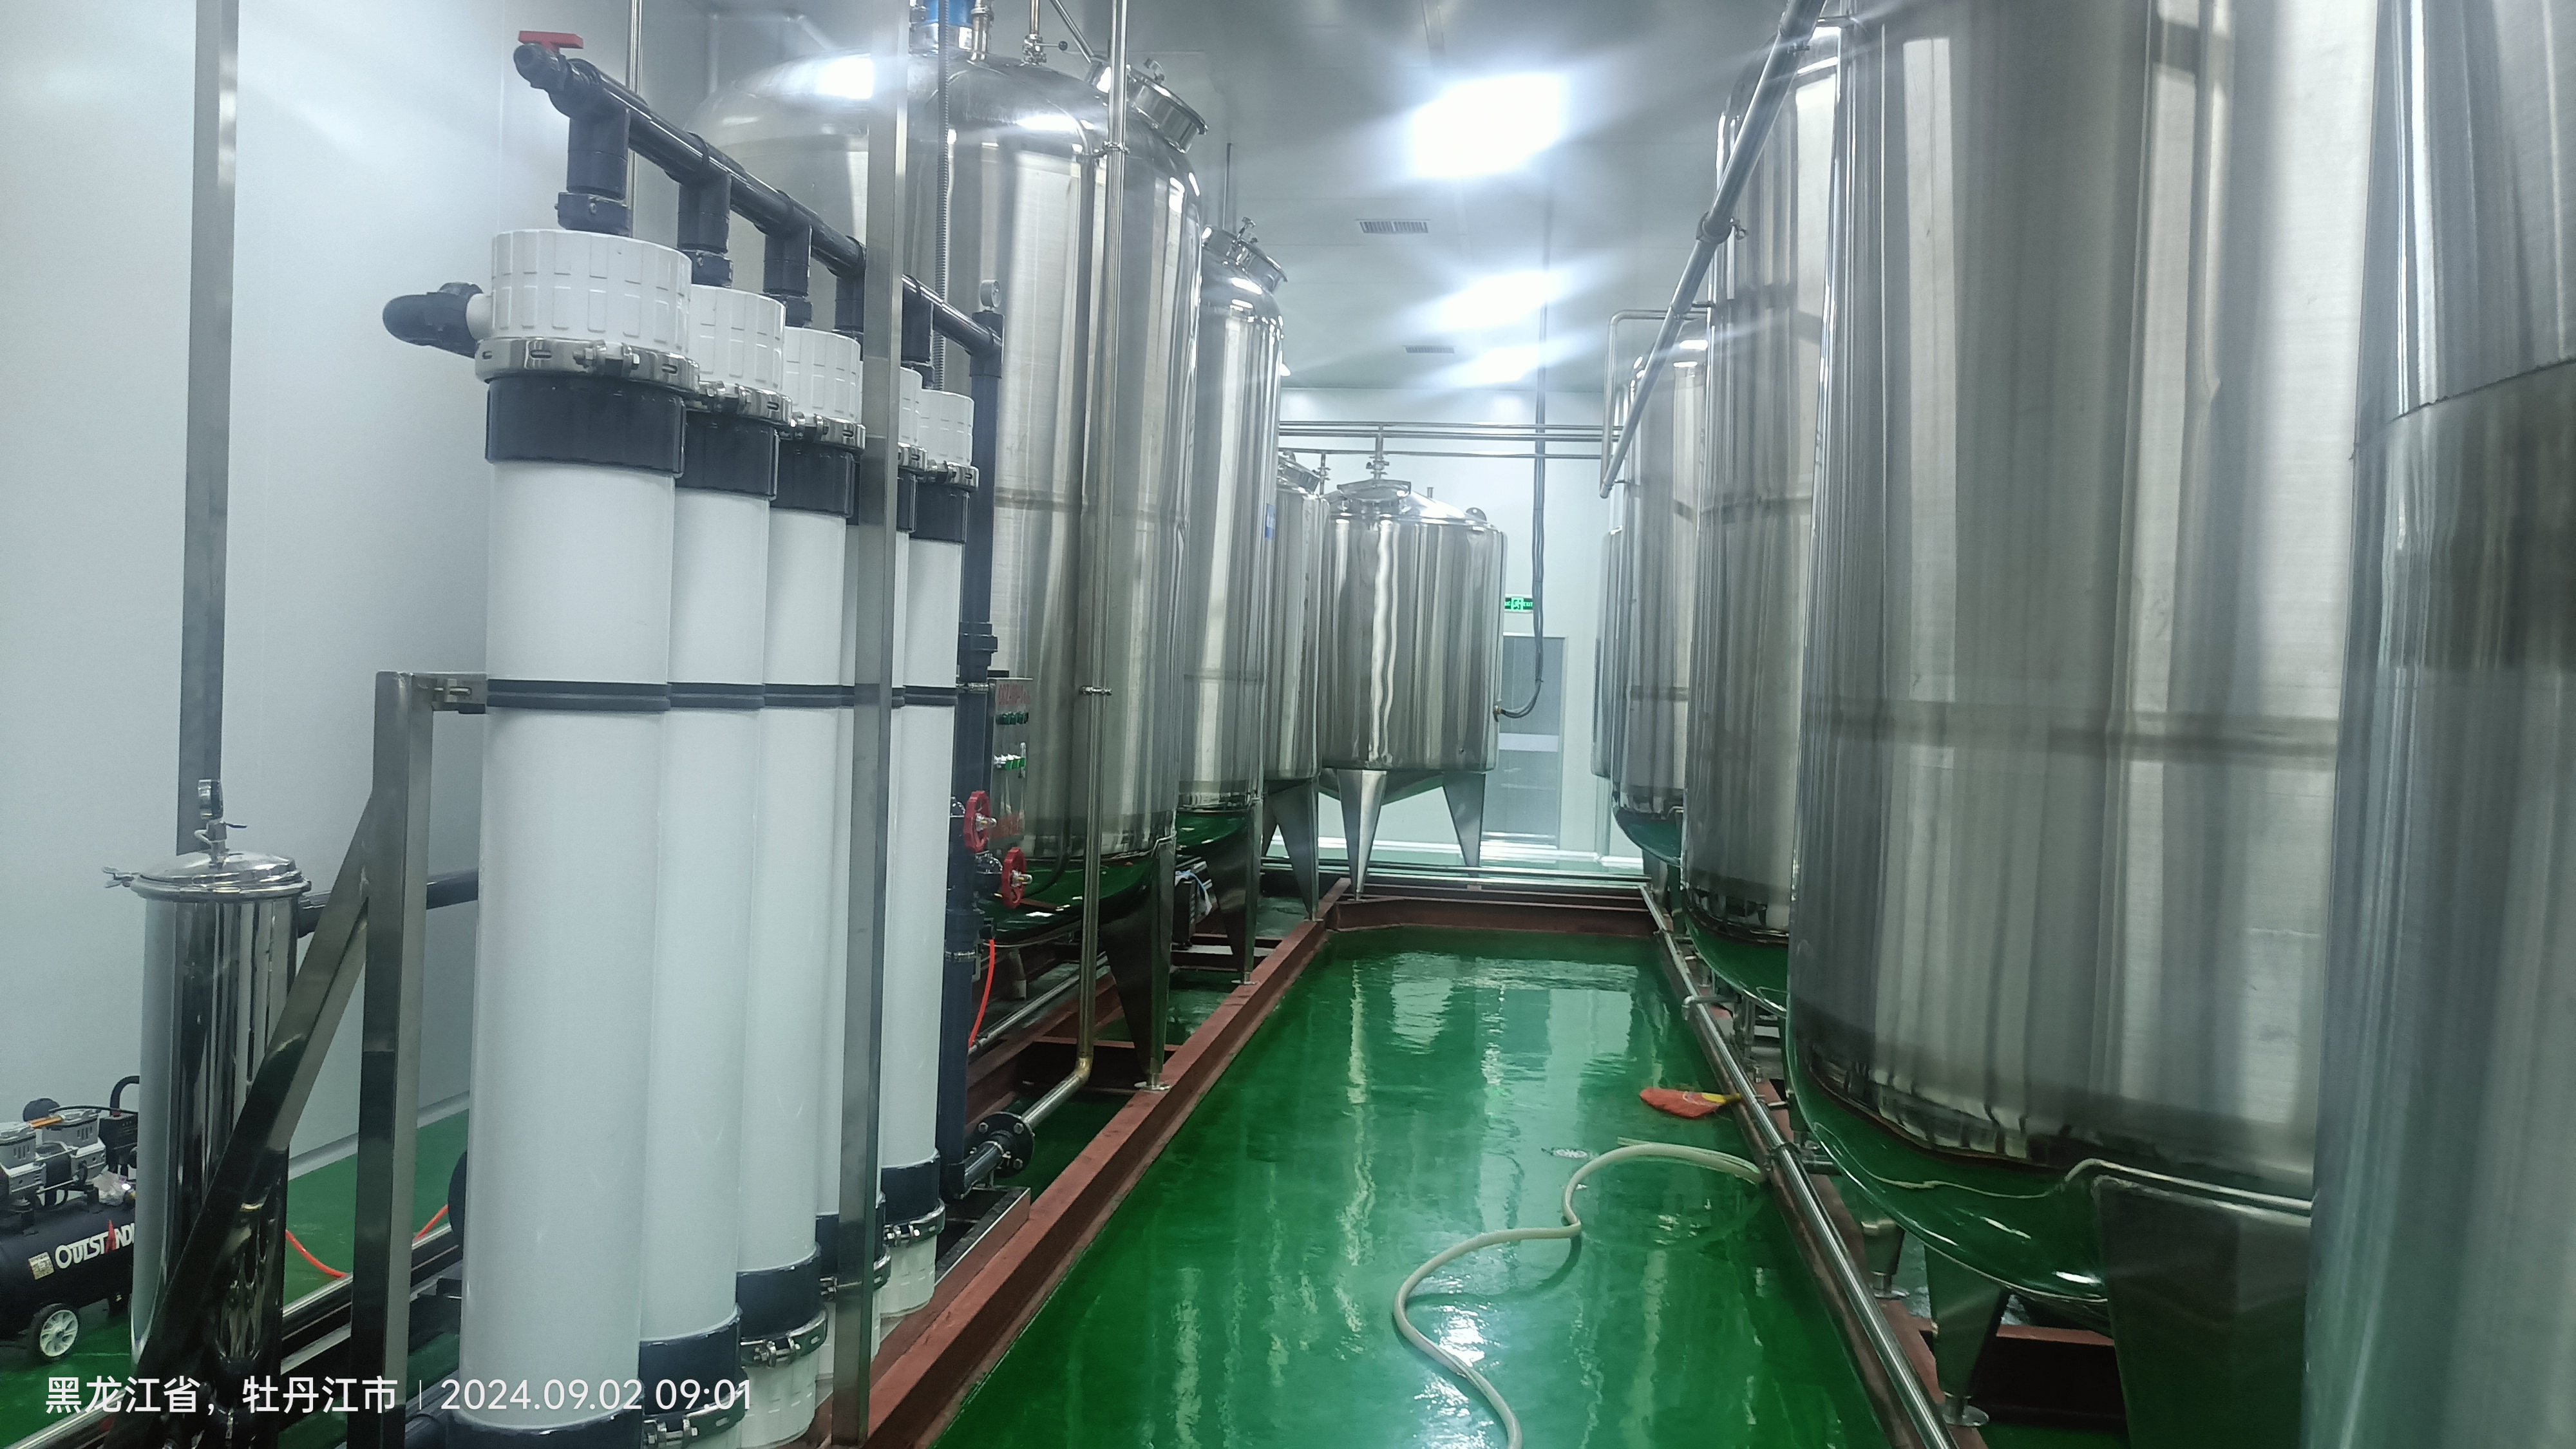
This turnkey system is designed for white vinegar production, covering alcoholic fermentation and acetic acid fermentation, including tank units, oxygen supply, temperature control, filtration and sterilization modules.
PRODUCT DESCRIPTION
Description
Our professional White Vinegar Making Equipment and Turnkey System is a fully integrated, automated production solution tailored for industrial-grade white vinegar manufacturing. Covering the entire production workflow from raw material pretreatment, alcoholic fermentation, acetic acid fermentation, precision filtration, sterilization to final product filling, this turnkey project delivers a one-stop factory solution for clients worldwide. It is applicable for mass production of food-grade industrial white vinegar, distilled white vinegar, and culinary white vinegar, widely used in food processing, catering, seasoning manufacturing, and daily chemical industries. Adopting mature aerobic acetic fermentation technology, the system realizes stable, high-efficiency, and low-consumption vinegar production, helping clients quickly launch standardized vinegar production lines with qualified final products.
2. Core Production Process
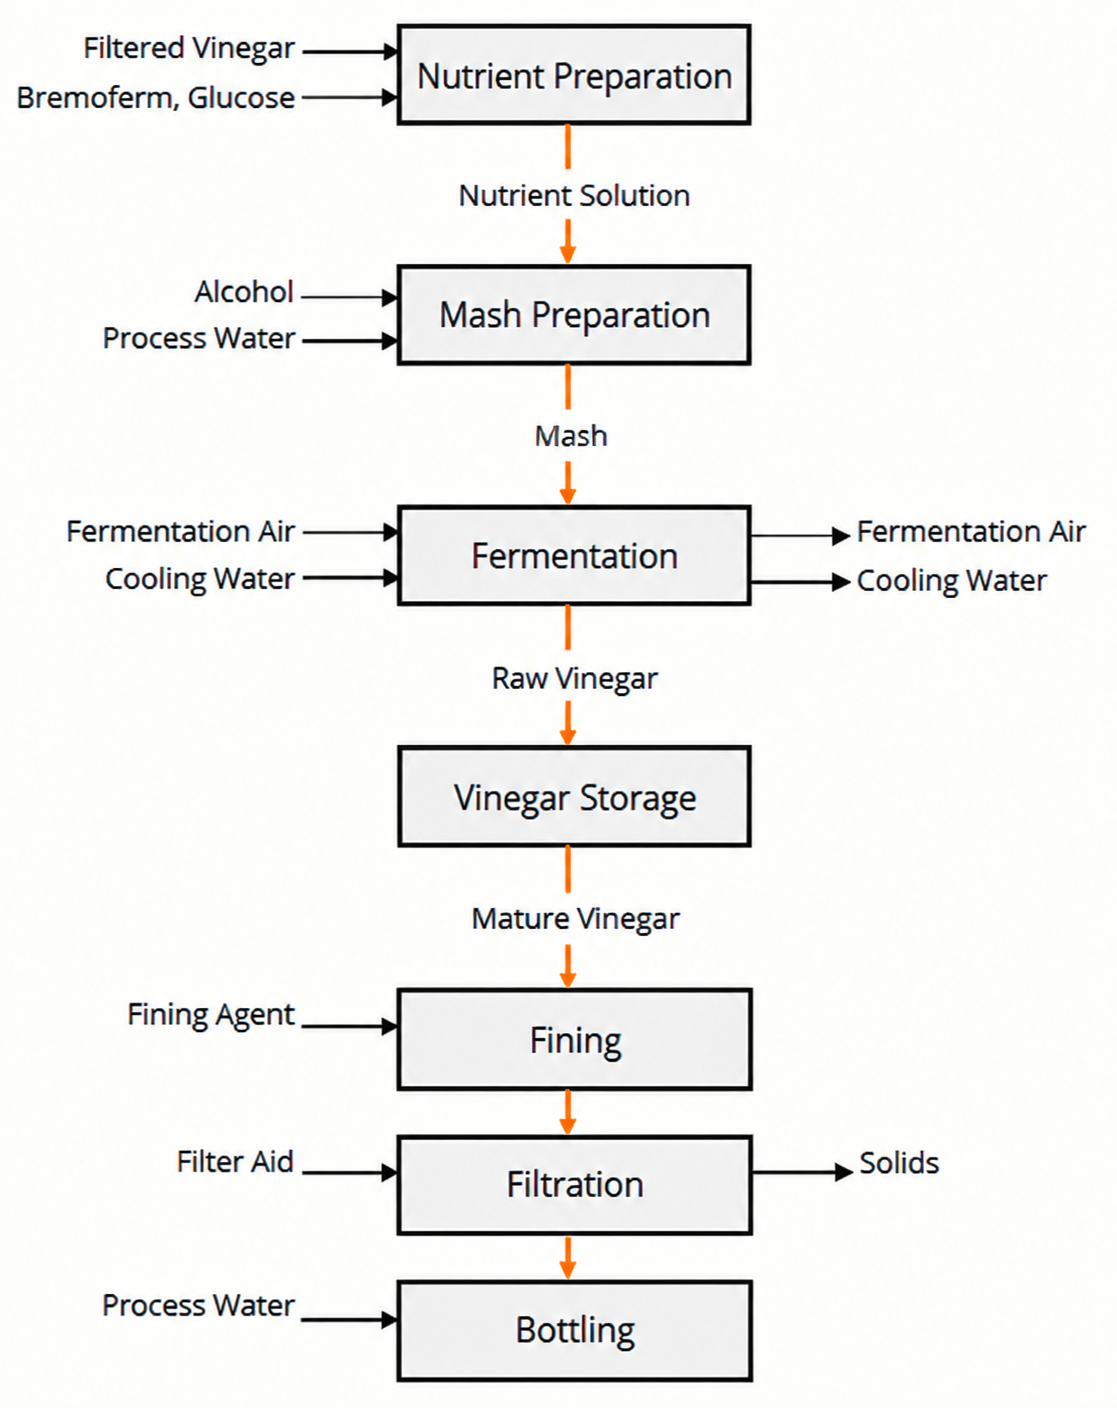
The complete White Vinegar Production Line strictly follows scientific two-stage fermentation technology to ensure high vinegar yield and pure taste, with the standard process flow as below:
Raw Material Preparation (glutinous rice, corn, alcohol, etc.) → Saccharification & Liquefaction → Alcoholic Fermentation (anaerobic fermentation) → Filtering & Purification → Aerobic Acetic Acid Fermentation → Vinegar Aging → Precision Filtration → High-temperature Sterilization → Homogenization → Final Filling & Packaging
The whole process realizes automated flow operation, effectively avoiding manual operation errors and ensuring consistent product quality in each batch.
3. Complete Equipment Configuration
Our turnkey system includes all core and auxiliary equipment required for white vinegar production, with full supporting facilities to realize unmanned automatic production:
● Raw Material Pretreatment Unit: Raw material cleaning machine, crushing equipment, saccharification tank, liquefaction tank, and mixing tank, realizing automatic batching and pretreatment of raw materials.
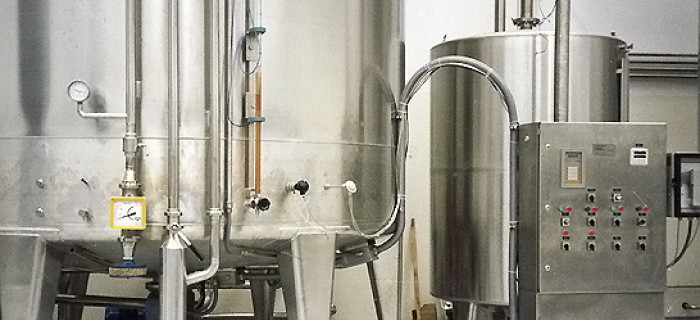
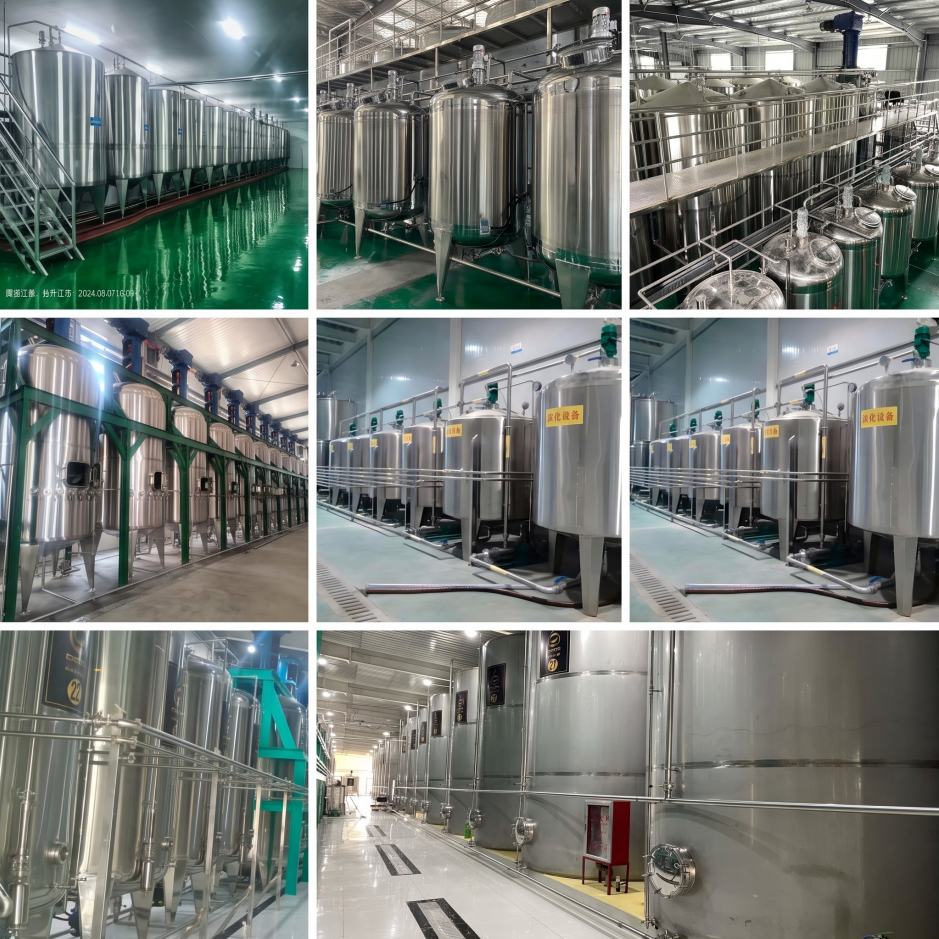
● Alcoholic Fermentation Unit: Vertical Stainless steel fermentation tanks with constant temperature control, sealed anaerobic fermentation structure, which improves alcohol conversion rate and avoids bacterial contamination.
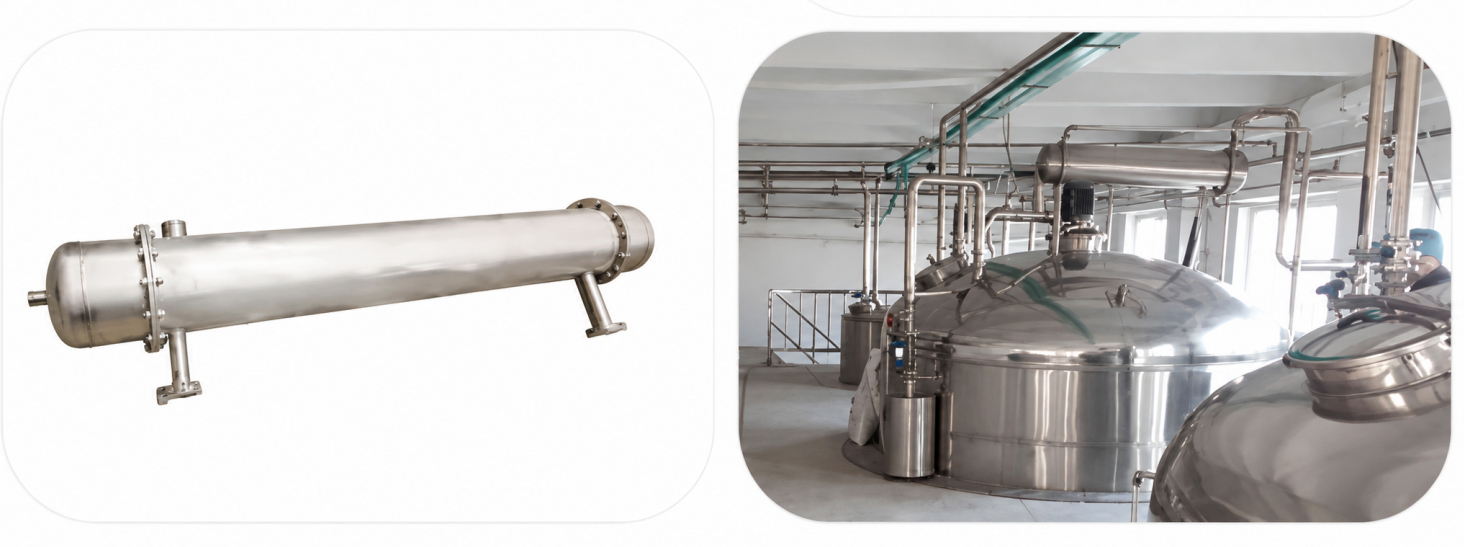
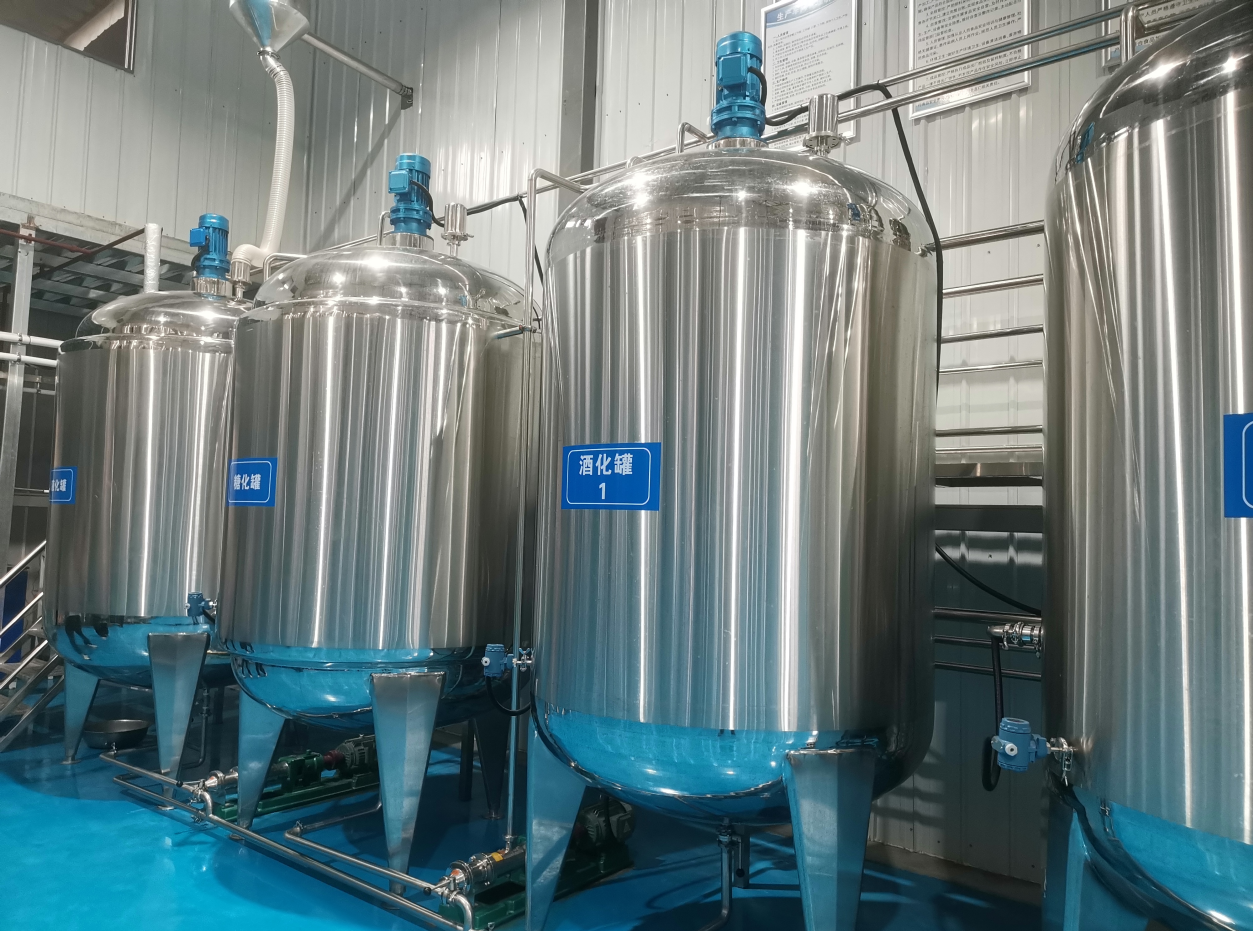
● Acetic Acid Fermentation Unit: Core aerobic fermentation tanks equipped with professional oxygen supply system, circulating stirring system, and intelligent temperature & pH monitoring system. It provides a stable growth environment for acetic acid bacteria and greatly improves acetic acid fermentation efficiency.
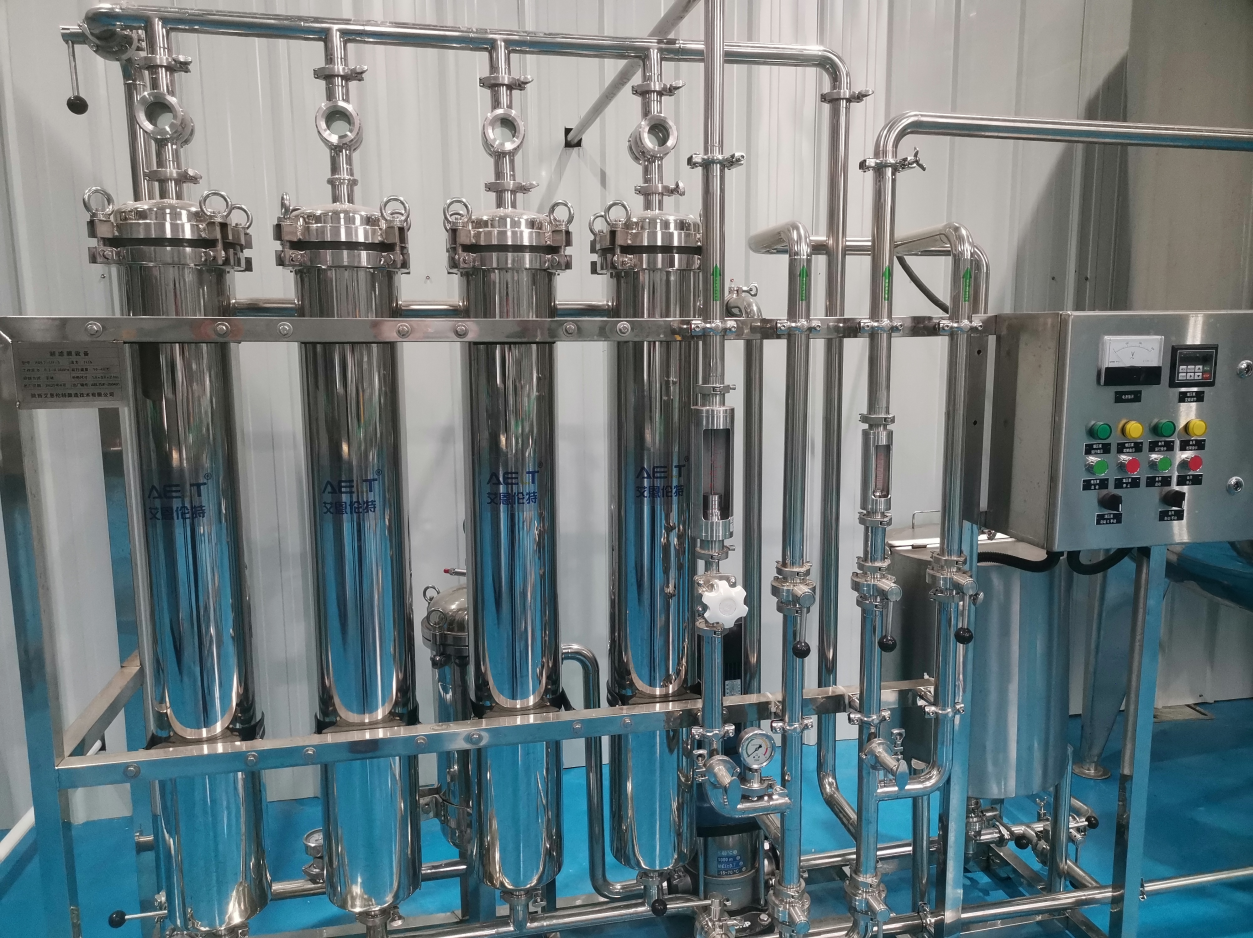
● Post-treatment Processing Unit: Multi-stage precision filter, diatomite filter, membrane filter, high-pressure homogenizer, and automatic sterilization machine, which remove impurities, precipitate and peculiar smell to ensure clear and transparent white vinegar with pure flavor.
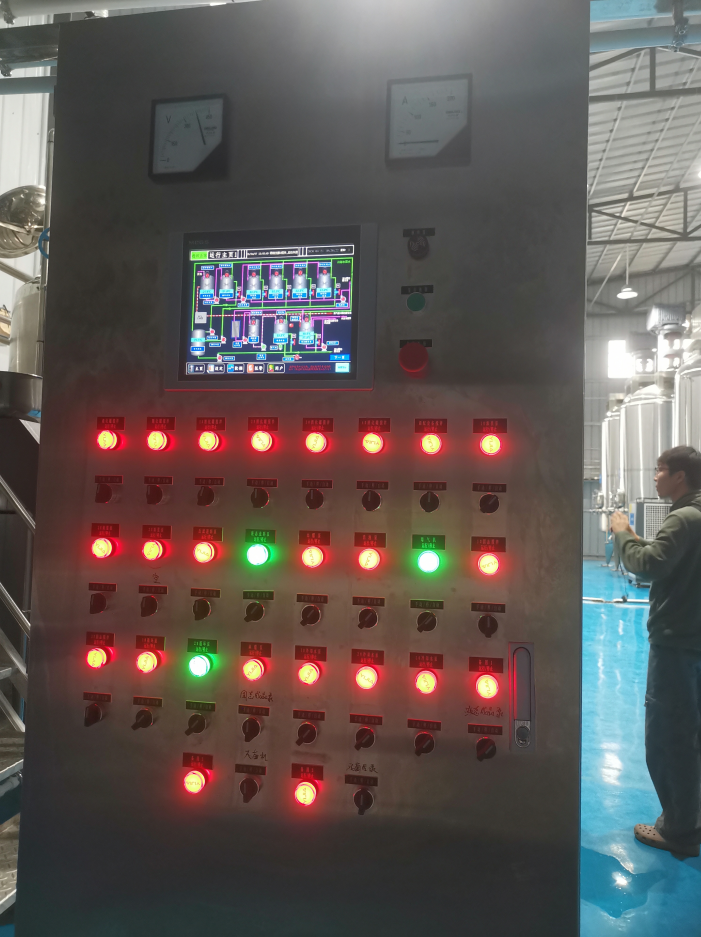
● Auxiliary Support Equipment: Cooling system, heating system, sterile air supply system, CIP automatic cleaning system, sewage treatment Supporting Equipment, and electrical control cabinet.
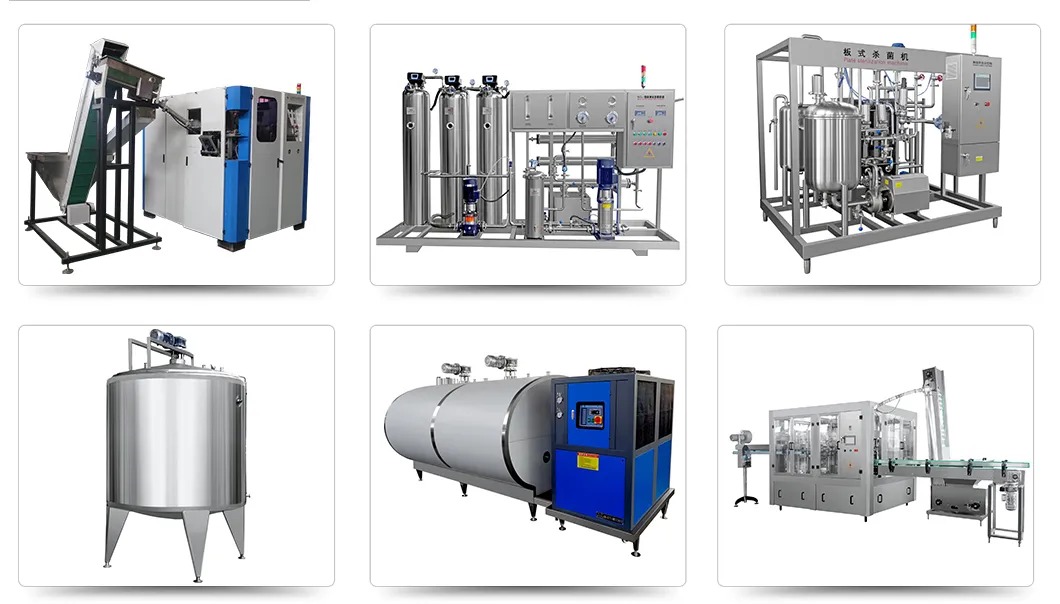
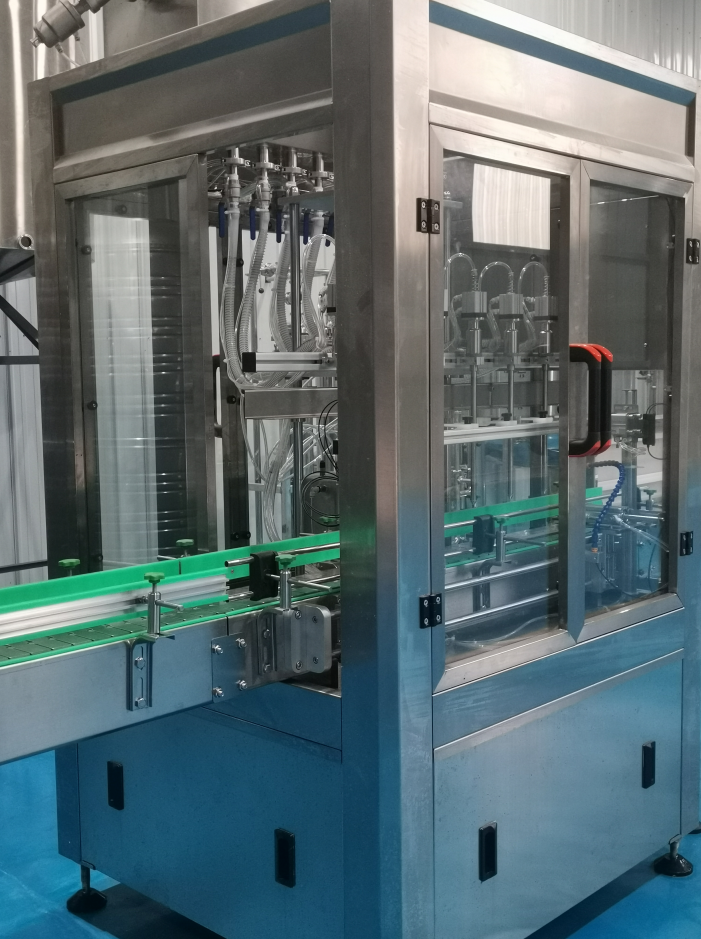
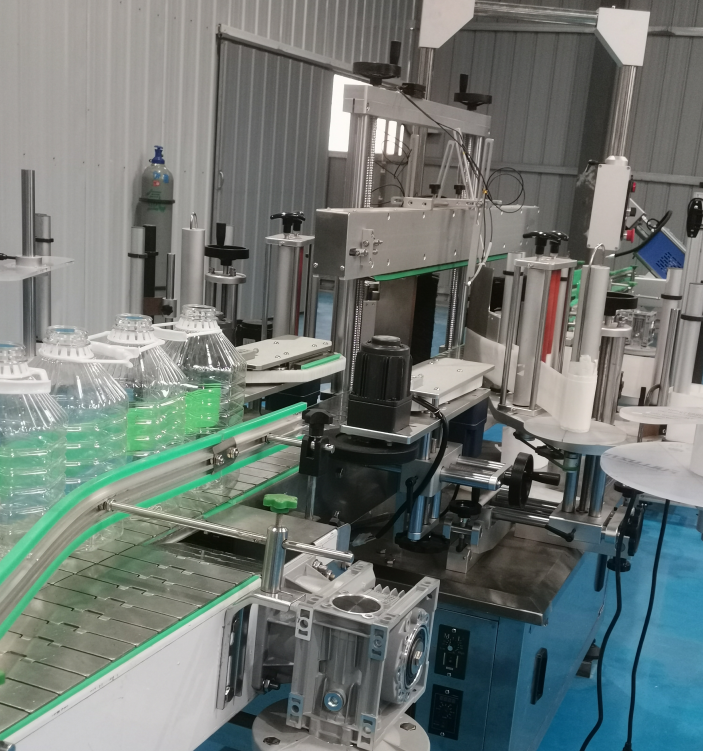
● Packaging Line: Automatic bottle washing, filling, capping, labeling, and packaging machines, realizing full-process automated production from raw materials to finished products.
4. Product Advantages
● High Fermentation Efficiency & High Yield: Optimized aerobic fermentation technology and intelligent oxygen supply control shorten the fermentation cycle, improve the conversion rate of raw materials, and increase the final vinegar yield by 15%-20% compared with traditional equipment.
● Full Automatic Intelligent Control: Equipped with PLC intelligent control system, it realizes automatic real-time monitoring and adjustment of temperature, oxygen volume, pH value, and fermentation time. The operation is simple, reducing manual labor cost and production error rate.
● Food-grade Safe Material: All tanks and pipelines in contact with materials are made of high-quality 304/316L stainless steel, which is corrosion-resistant, high-temperature resistant, easy to clean, and meets international food safety standards.
● Low Energy Consumption & Environmental Protection: Equipped with energy-saving heating and cooling circulation system, which reduces energy consumption. The matched sewage treatment system ensures that production wastewater meets environmental discharge standards, realizing green production.
● Stable Product Quality: Standardized closed fermentation production avoids secondary pollution. The produced white vinegar is clear and transparent, with moderate acidity, pure taste, no peculiar smell, and stable batch quality.
● Flexible Customization: We support customized production lines with different capacities (1 ton - 100 tons per day) to meet the production needs of small, medium and large vinegar factories.
5. Technical Parameters (Optional Customization)
● Daily Production Capacity: 1T/D ~ 100T/D (customizable)
● Fermentation Tank Volume: 500L ~ 50000L
● Applicable Acidity Range: 3% - 30% edible white vinegar
● Control Mode: PLC full automatic intelligent control
● Material of Main Equipment: SUS304/SUS316L stainless steel
● Fermentation Cycle: 7-15 days (adjustable according to capacity and process)
● Product Purity: Meet international food-grade standards
6. Turnkey Service Scope
As a professional turnkey system supplier, we provide full-cycle one-stop services without intermediate links, allowing customers to start production quickly after project delivery:
● Professional production process design and factory layout planning according to customer site and capacity requirements
● Full set of equipment manufacturing, processing and quality inspection
● On-site installation, commissioning and equipment debugging
● Professional operation training, maintenance training and production process guidance for workers
● Complete project acceptance and production handover
● Long-term after-sales service, equipment maintenance and spare parts supply
7. Application Scope
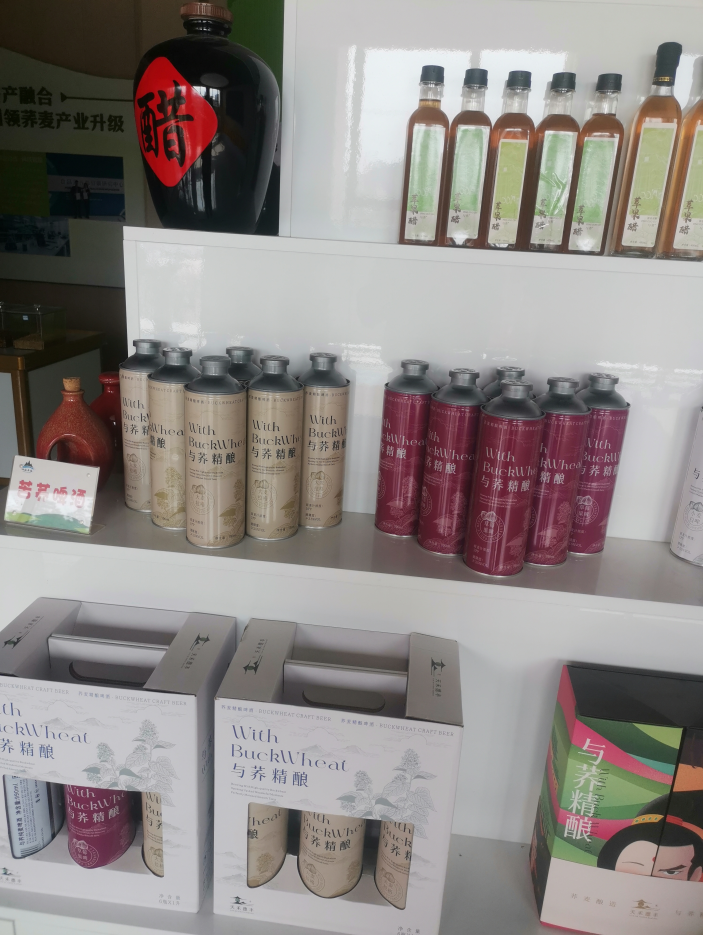
This turnkey system is widely used for the production of edible white vinegar, industrial white vinegar, distilled vinegar, synthetic vinegar and other vinegar products. The finished products are widely used in food seasoning, pickling processing, beverage production, daily cleaning, pharmaceutical and chemical industries, with broad market application prospects.
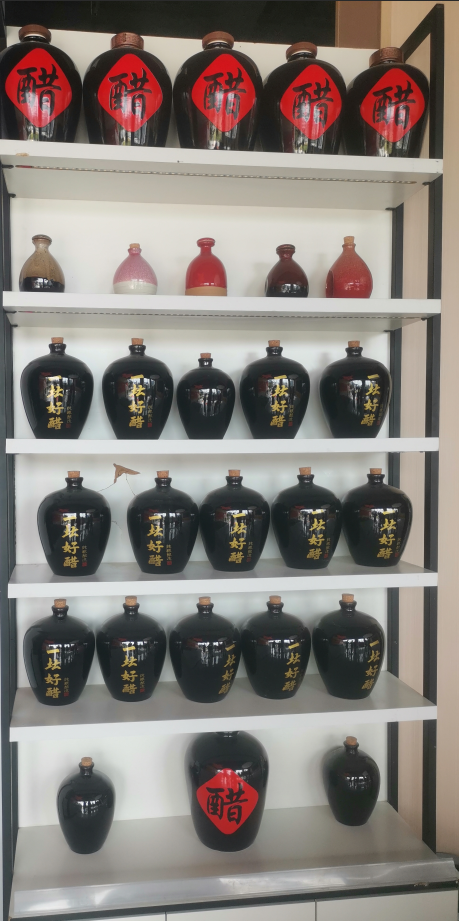
Project Cases
Complete White Vinegar Technology Guide
White vinegar (also known as alcohol-based vinegar) is produced from diluted neutral alcohol. It is widely utilised as an acidulant and preservative within the food-processing industry.
We deliver process design and equipment for vinegar production for capacities starting from 4,000 litres per day.
Key Figures for Vinegar Plant Construction
Block Diagram
Aelt Process for Vinegar Production from Pure Alcohol
Acetic acid bacteria convert ethanol into vinegar. Following a maturation phase, the vinegar must be clarified via clarification and filtration steps.
Mash Preparation
Raw-Material Handling
Inside the feed tank, pure alcohol is diluted with process water to a maximum concentration of 15 % and mixed with raw vinegar containing acetic acid bacteria. Nutrients and a small volume of vinegar are blended in a nutrient vessel before being transferred into the feed tank for further dilution and mixing.
This mash is prepared in batches one to two times per week in one feed tank, while a second feed tank serves as the supply reservoir for fermentation.
Vinegar Fermentation
Bioreaction
Fermentation is operated in semi-continuous mode. The alcoholic mash is aerated inside the fermenter by our proprietary IP-8 self-priming aeration system. The fermentation cycle terminates when the vinegar concentration reaches its maximum and the alcohol content drops to approximately 0.3% by volume. Then around one-third of the contents in the fermenter are pumped to the discharge tank.
The fermenter is replenished with fresh mash from the injection tank for the next fermentation batch. One batch cycle takes roughly one day, with the exact duration subject to the alcohol content of the raw material.
Nutrients Aelt
Nutrients are essential for optimal growth of acetic acid bacteria. Nutrient blends are selected according to raw-material type to improve substrate nutritive value and raise process yield.
For white-vinegar production, glucose together with Acetic acid bacterial nutrient blend a proprietary formulation rich in vitamins, minerals and other nutritional components — is added to the mash.
Maturation, Clarification and Filtration
Product Separation & Polishing
Freshly produced raw vinegar drawn from the fermenter undergoes maturation over several weeks inside the discharge tank. During maturation, turbidity-causing impurities such as bacteria, coagulated proteins and precipitated salts settle at the tank bottom.
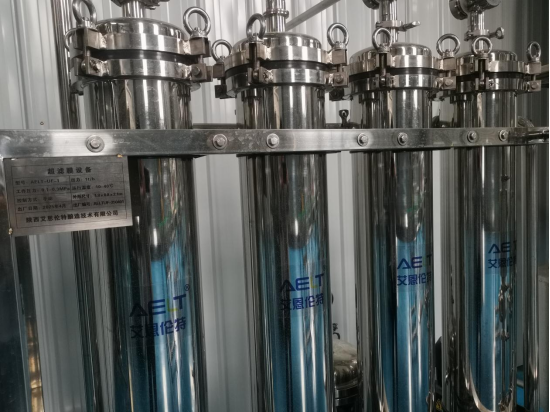
If required, clarifying agents may be dosed in dedicated clarification tanks for further polishing of raw vinegar. Matured vinegar passes through filtration modules to remove residual solids. Prior to bottling or bulk loading, it goes through sterile-grade filtration and is diluted with process water to target concentration.
Production Capacities
Standard Plant Sizes
Fermenter Type | ALT300 | ALT600 | ALT1200 | ALT2400 |
Volume (m³) | 18 | 36 | 72 | 144 |
Capacity (10 % vinegar, L/day) | 4 000 | 8 000 | 15 000 | 30 000 |
Cooling-water duty at 24 °C (m³/h) | 20 | 40 | 80 | 160 |
Typical footprint (m²) | 300 | 400 | 600 | 800 |
Minimum building height (m) | 7.6 | 7.7 | 9.5 | 10.5 |
Fully-Automated Fermentation
Process Control
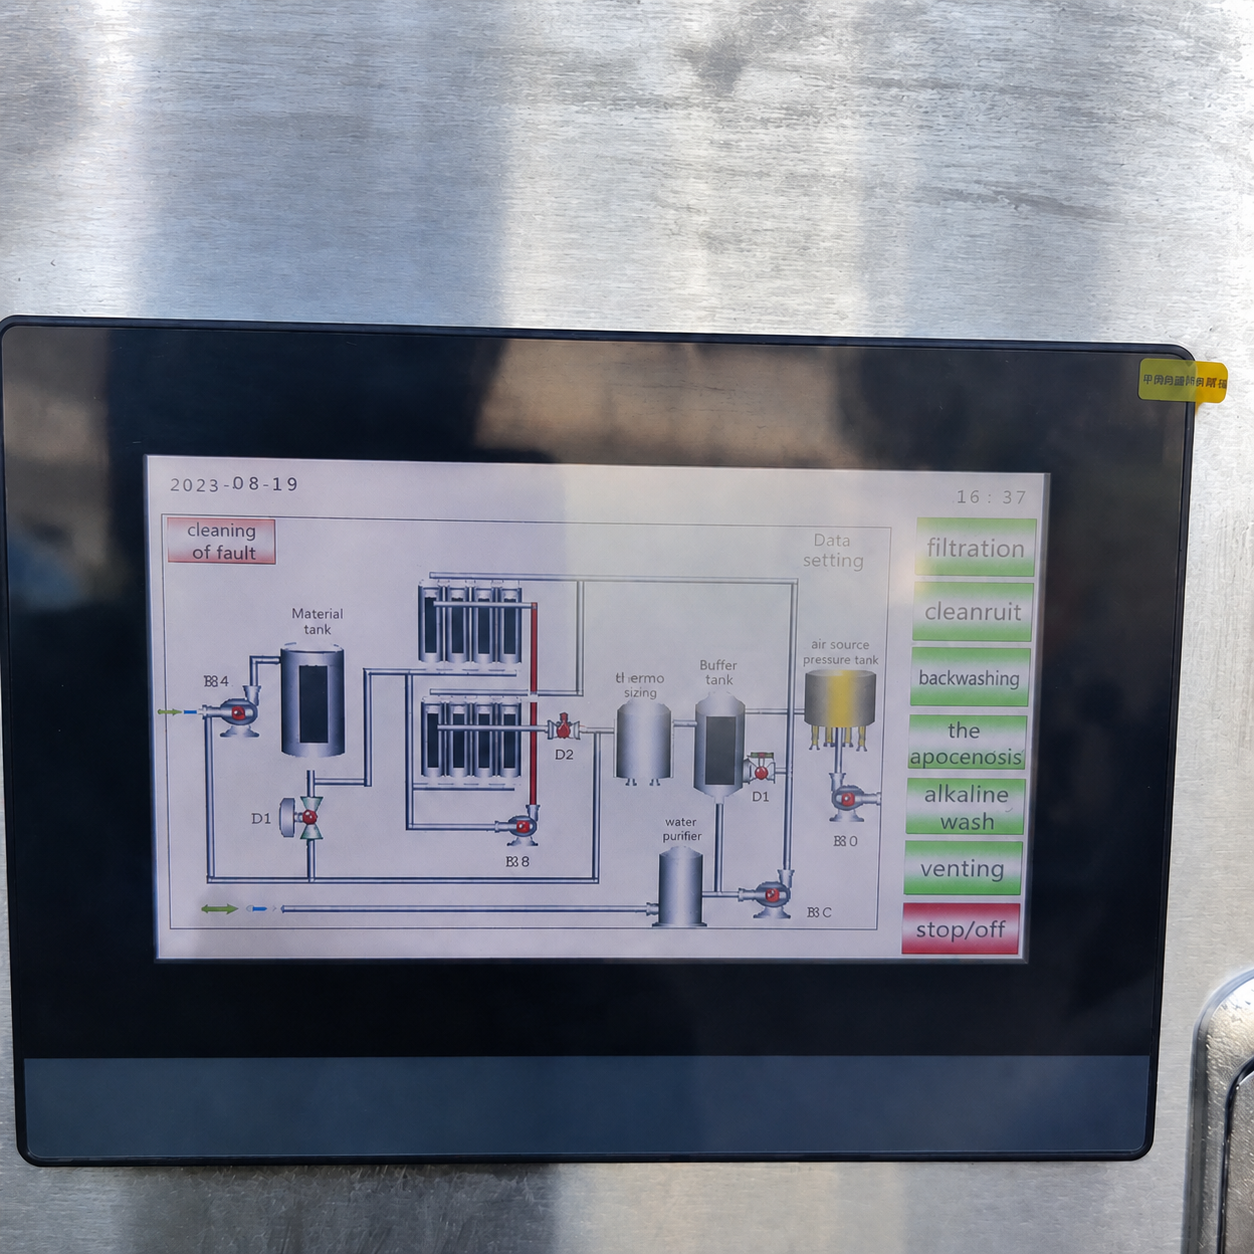
Aelt fully-automated vinegar fermentation incorporates sensor-equipped measuring systems for on-line alcohol-content monitoring of fermenting mash.
Alcohol concentration is continuously tracked throughout fermentation. When the preset residual alcohol level is reached, raw vinegar is discharged automatically and fresh alcoholic mash refills the fermenter.
Emergency power supply with auto-start capability guarantees uninterrupted fermentation in case of power outages.
Custom-Engineered Solutions
Our services can be tailored to your requirements. We offer design and supply ranging from key components (fermenters, aerators and process-control systems) up to full-scope EPC solutions for complete production lines including instrumentation & control and laboratory equipment.
Our specialists can also upgrade or revamp existing facilities and integrate vinegar-production units into other manufacturing sites, such as alcohol-production plants.
Cooling Requirements
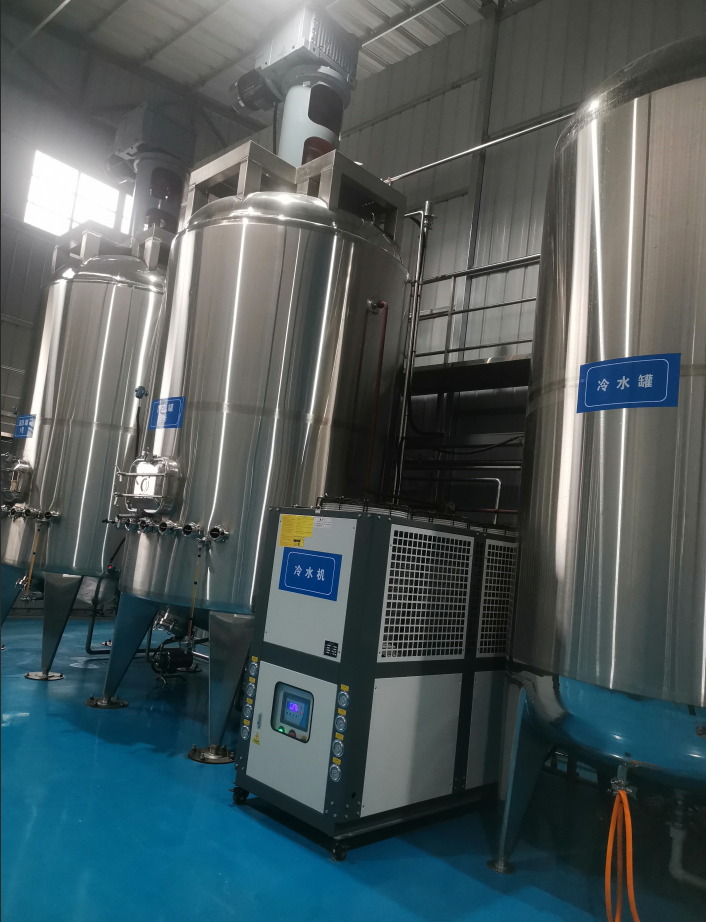
Fermentation is an exothermic reaction, making cooling critical for stable operation. Cooling water supplied at 24 °C (returning at 27 °C) removes process heat and is decisive for reliable vinegar manufacturing.
Aelt proprietary design features finely balanced internal cooling-coil assemblies installed inside fermenters. (Image: interior view of fermenter vessel.)
Typical Utility Consumption for White Vinegar Production
All figures given are typical values and subject to variation based on plant layout and equipment configuration.
White Vinegar (Alcohol-Based)
Our Reference Vinegar Projects
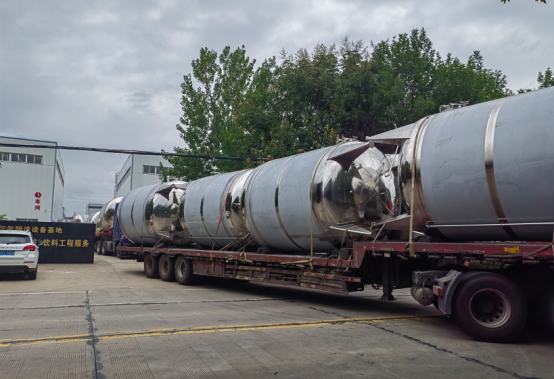
Vinegar Fermenter for Algeria, Vienna, Austria.
Delivery of one Type 1200 vinegar fermenter fitted with IP-8 self-priming aeration system. Rated capacity: 15 000 L/day (10 % vinegar), designed for processing pure ethanol, grape wine and apple wine.
Frequently Asked Questions
All information provided represents typical values and may differ according to individual plant configuration. Please send us your project specifications for detailed information.
· What is the recommended minimum plant capacity?
· What investment is required to build such a plant?
· What maximum acetic-acid concentration can be achieved?
· What constitutes Aelt’s minimum scope of supply?
· Can Aelt aerators be retrofitted into my existing fermenter vessels?
· Why do I need an emergency power supply?
· Why are nutrients required for this process?
· How can I obtain further information for my vinegar-plant project?
 +86 29-87031531



 핸드폰